Opening note and industry anchor
We begin plain — precision wins projects. From small municipal parks to big names like Atlantis The Palm’s Aquaventure in Dubai, the difference between a slide that lasts and a slide that fails often sits in millimetre-level decisions. This piece compares how leading water park manufacturers and contractors set thickness tolerance, choose polymer formulation, and control finish quality. For operators and specifiers who deal with design loads and maintenance cycles, these details matter to lifespan and uptime.
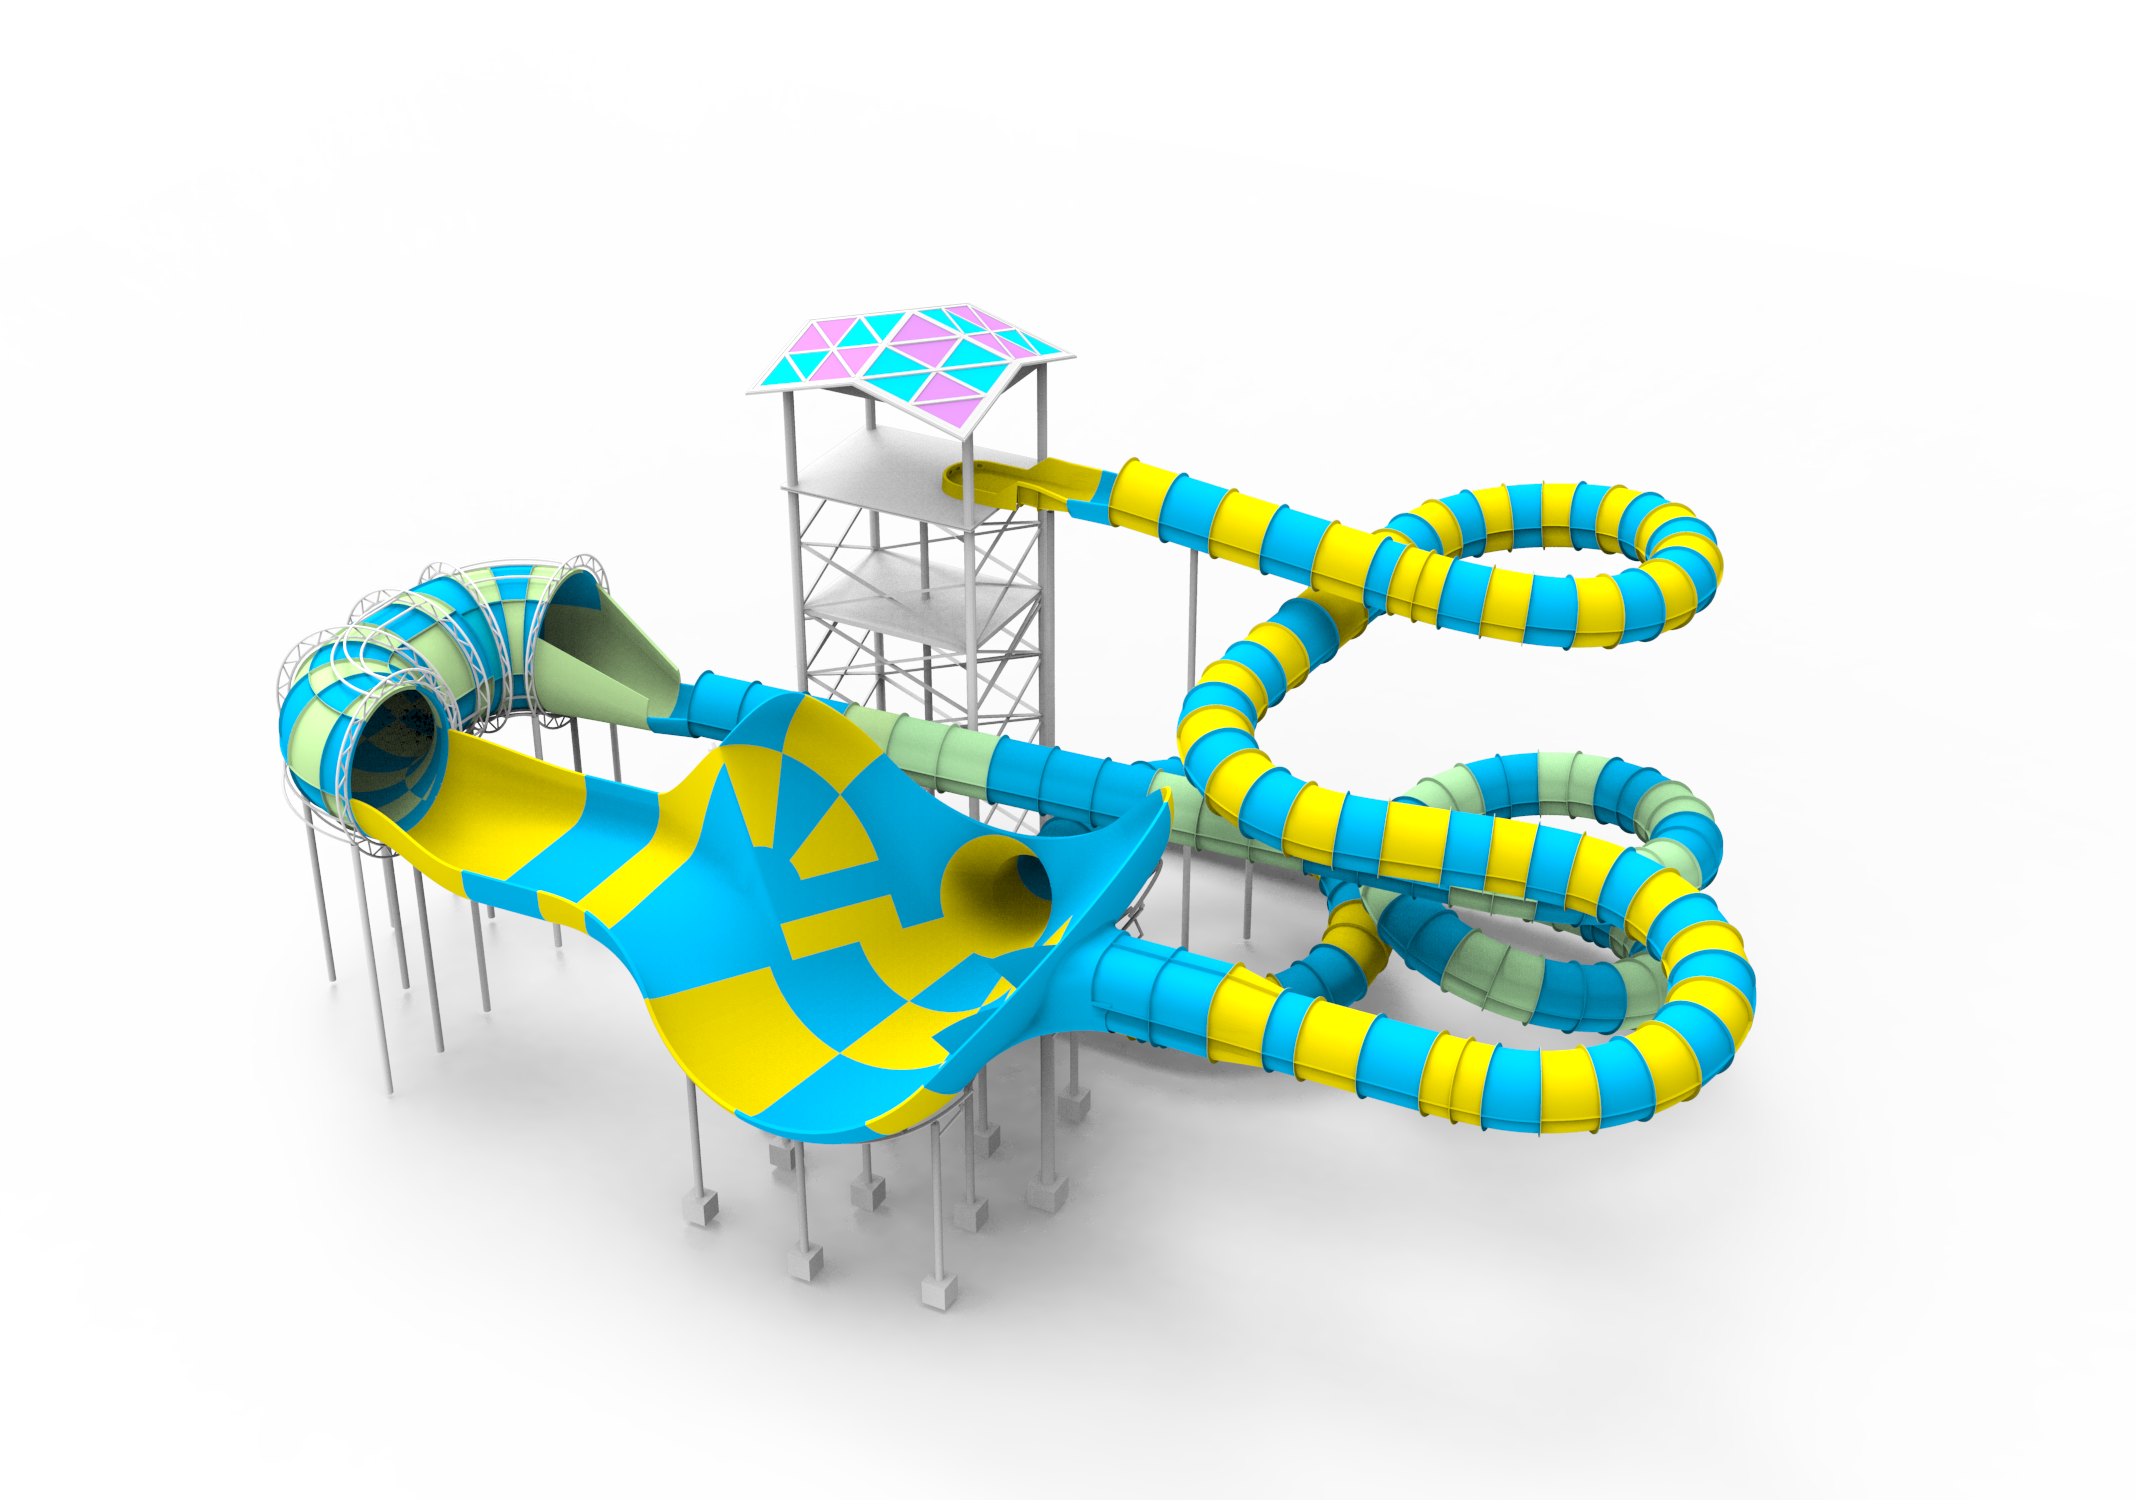
Why thickness and molding precision determine long-term value
Thickness tolerance is not an aesthetic tick-box — it governs structural strength, impact resistance and how a gelcoat finish adheres. When a fiberglass reinforced plastic (FRP) shell carries dynamic loads from riders, a consistent wall thickness prevents stress concentrations and delamination. Precision molding locks in repeatability: same mould, same cure time, same polymer formulation. That repeatability reduces warranty claims and keeps throughput predictable for owners.
How manufacturers turn specs into repeatable parts
Top shops use a recipe of tooling discipline and testing. Rotational molding or matched-die molding is set with controlled cure cycles and documented thickness checks across defined sections: apron, chute, transition and bowl. Non-destructive ultrasonic gauging and destructive coupon testing during pilot runs confirm actual versus nominal. Hydrodynamic profiling and surface finish — measured as Ra values for slipperiness — complete the package. These processes feed QA sign-offs before components ship to the site.
Side-by-side: supplier practices that separate good from great
Compare three practices that matter: tooling stability, polymer traceability, and post-cure dimensional checks. Some firms rely on hand-layup for bespoke shapes; others push automated gelcoat spray and vacuum consolidation to control resin distribution. The best ones keep certified lot records for resin and catalyst, plus torque-specified stainless steel anchor bolts for assembly. Where contractors partner closely with manufacturers — especially with experienced water park construction companies — installation gaps shrink and commissioning moves faster.
Operational production teardown — what to inspect on arrival
When pallets arrive, target three zones: transitions, joints and bolt flats. Measure local thickness at designed reference points; compare to drawing callouts. Inspect gelcoat for consistent cure colour and for micro-cracking. Check how joint flanges mate — alignment tolerances should match spec. Also, embed procurement records into handover: batch numbers, cure profiles, and test certificates. For clarity, list {main_keyword} and {variation_keyword} in the production log so contractual scope & warranty triggers are traceable.
Common mistakes that trip projects
Teams often underestimate environmental cure effects — humidity can extend cure time and reduce crosslink density, especially with accelerated catalysts. Another trap: relying solely on visual inspection for wall thickness. Ultrasonic or destructive coupon checks catch hidden thin spots. And installers who skip a dry-fit before final bolting invite alignment stress. These are avoidable with clear handover protocols — and regular site audits during the first months of operation. — A quick note: maintenance plans must reflect material choices; FRP patches differ from thermoplastic repairs.
Advisory: three golden rules for selecting builders and materials
1) Verify documented thickness tolerances and acceptance ranges per component; require spot-check reports from independent labs during pilot production. Measurement should specify gauge positions and sampling frequency.
2) Demand material traceability: resin lot, gelcoat batch, catalyst profile and cure schedule. Those items predict long-term UV and chlorine resistance better than marketing claims.
3) Insist on integrated testing: load tests on assembled sections, ultrasonic thickness mapping, and finish slip trials under expected water chemistry. Include remediation steps and response times in contract.
Final practical rhythm: choose partners who show their process on paper and on the mould floor — that foresight buys seasons of trouble-free operation. Dalang. –